Reusable Formwork
Greater efficiency in the use of natural resources, due to its reusable nature, the reduction in the consumption of concrete and timber, and the fact that it contains recycled material in its composition.
Principles
The FGM mould system is based on principles of economic rationalisation that allow the construction of one-way or two-way ribbed slabs commonly referred to as lightweight flat slabs. It was designed not only to reduce construction resource consumption but also with a view to reuse and rotation of the equipment needed for slab construction, with significant benefits in terms of concrete and steel consumption as well as reduced formwork equipment immobilisation and labour requirements.
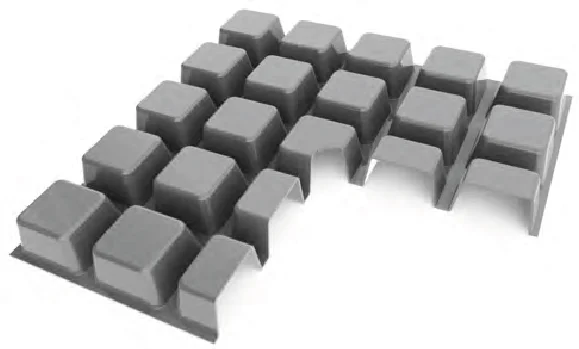
The use of the FGM mould system guarantees:
- Recovery of formwork equipment by the end of the third day after slab casting
- Construction of large-span slabs with low concrete consumption
- Economy in vertical elements due to load reduction
- Reduced need for specific punching shear reinforcement
- Compatibility with any formwork support system
- Greater efficiency in the use of natural resources, due to its reusable nature, the reduction in concrete and timber consumption, and the fact that it contains recycled material in its composition
FG600 Moulds
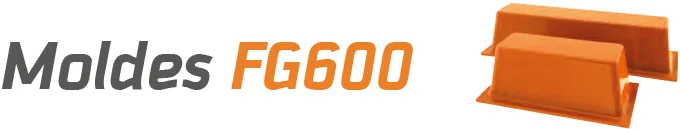
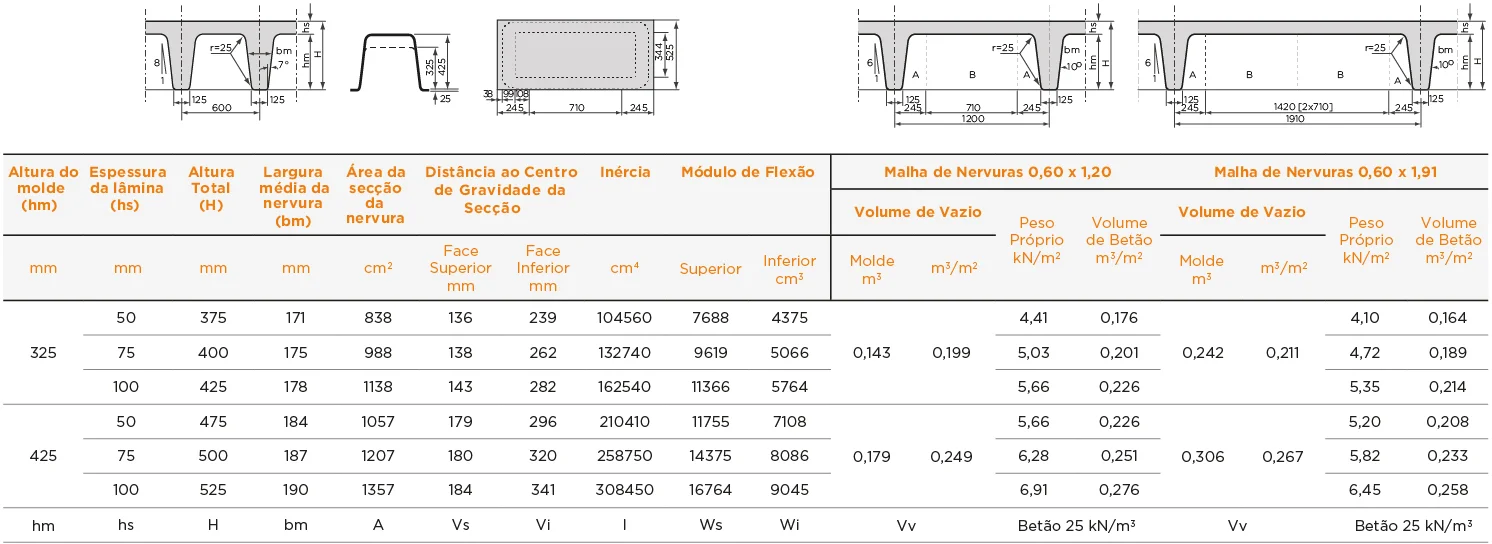
The FG600 moulds were designed for the construction of one-way slabs, enabling a reduction in material consumption while maintaining high inertia in the dominant direction. The moulds consist of the combination of two types of element — the top and the centre — allowing various configurations. The grid resulting from the use of these moulds has a centre-to-rib spacing of 0.60 m in the main direction and 1.20 m, 1.91 m or 2.62 m in the other direction; in both directions the rib base is 0.125 m. FG600 moulds are available in heights of 0.325 m and 0.425 m.
Note: These moulds allow the inclusion of any number of units identified as type B, giving complete mould lengths of 1.91 m, 2.62 m, 3.33 m, 4.04 m. The values shown refer to the slab cross-section between rib centrelines.
FG800 Moulds
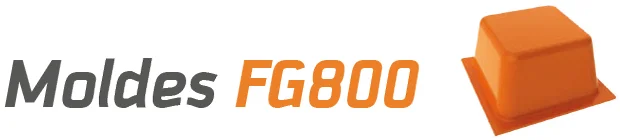
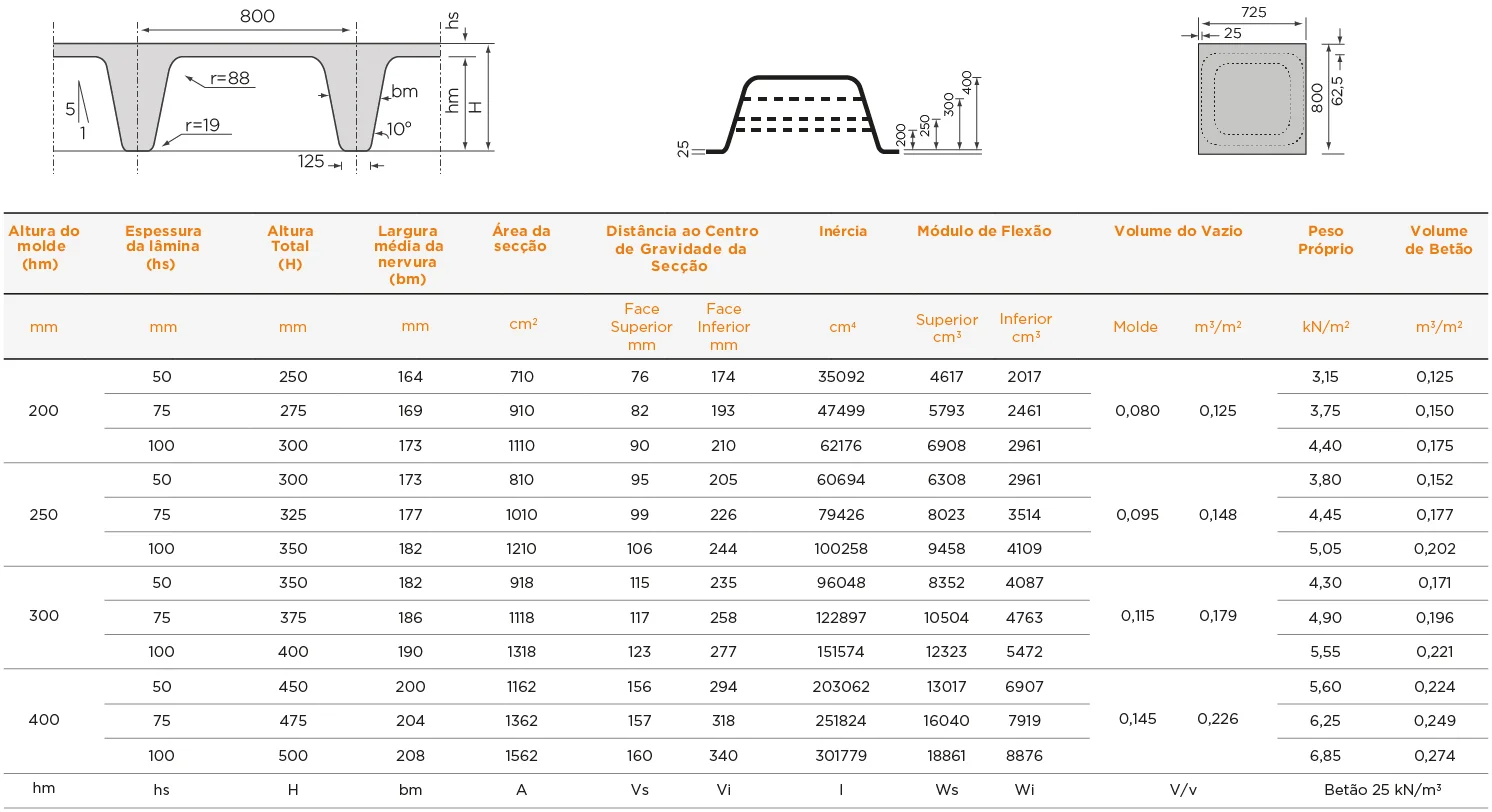
The FG800 moulds for two-way slabs have a rectangular plan shape with dimensions of 0.80 m × 0.725 m, forming a 0.80 m rib-centreline grid when the shorter flange rests on a 0.075 m ledger. In terms of void height, four different sizes are available: 0.20 m, 0.25 m, 0.30 m and 0.40 m.
Note: For application on continuous decking or directly on the primary formwork structure, square moulds designated Q800 can be produced with the same void heights. The values shown refer to the slab cross-section between rib centrelines.
FG900 Moulds
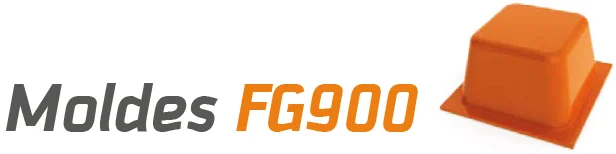
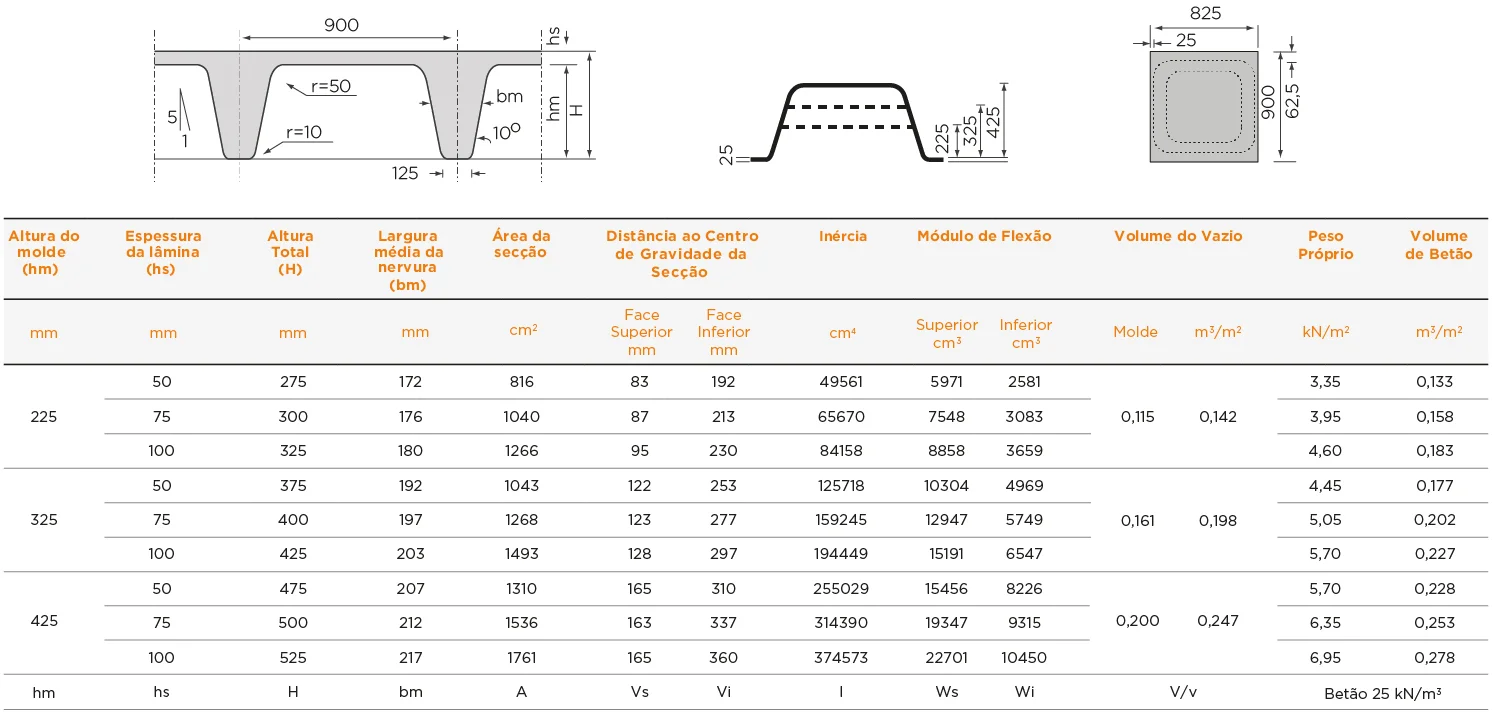
The FG900 moulds for two-way slabs have a rectangular plan shape with dimensions of 0.90 m × 0.825 m, forming a 0.90 m rib-centreline grid when the shorter flange rests on a 0.075 m ledger. In terms of void height, three different sizes are available: 0.225 m, 0.325 m and 0.425 m.
Note: For application on continuous decking or directly on the primary formwork structure, square moulds designated Q900 can be produced with the same void heights. The values shown refer to the slab cross-section between rib centrelines.
Execution
Ferca also offers a complementary formwork system that optimises the FGM mould system on any formwork support structure. This system consists of rails and head pieces which, supported on the primary structure, allow the removal of all equipment on the 3rd day after casting, retaining only the re-propping required at this stage of construction.
Assembly of the support structure
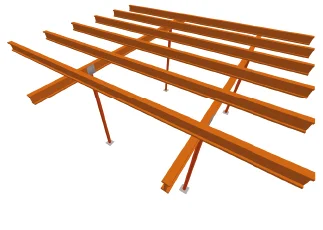
Installation of rails, head pieces and props
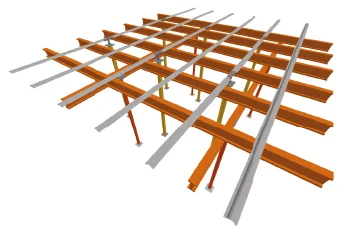
Placing of plastic moulds
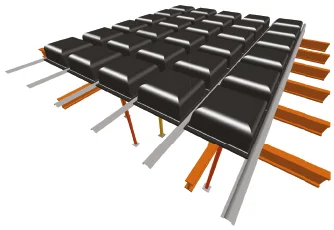
Slab casting
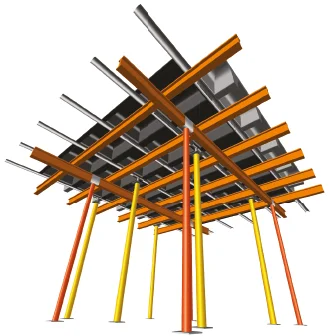
Recovery of all equipment on the 3rd day
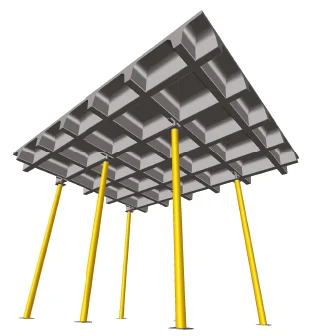
Finishing
The concrete surfaces in contact with the moulds are very regular and generally require no further finishing. Special attention should be paid to the joints between moulds and between the moulds and the support structure, where it may sometimes be necessary to remove irregularities to obtain a better final finish.
Preparation for Casting
All propping should be properly braced and the moulds tightened together to eliminate any movement, while also ensuring a better surface finish. It is also advisable to spray the moulds with a release agent prior to casting.
Mould Removal
Immediately after stripping, the moulds should be cleaned with water and non-abrasive materials. When stripping, the corners should not be forced nor should the moulds be dropped; in the event of breakage they should be returned for repair. When not in use, moulds should be stored upright, stacked and supported on the wider flange.
Fire Resistance
For calculating the fire resistance of the cross-sections shown in the tables above, the parameters defined in current regulations should be analysed. Through the definition of slab geometry, fill and cover depths, it is possible to achieve a fire resistance of 2 hours.
Downloads
Contacts
Write to us. Present us a challenge.
Message sent successfully. Thank you!